In the fast-changing world of material handling, you really can’t underestimate how important a dependable bucket elevator is. Industry pro John Smith, who's a top consultant at Conveyor Systems Ltd., once said, "A well-designed bucket elevator can seriously boost how smoothly your operations run." That little quote really puts into perspective how crucial it is to pick a quality product when it comes to elevators.
Lately, the Chinese market has been buzzing with a rise in high-quality, custom-made bucket elevators. It’s great because now there are tons of options that fit different industrial needs. Companies are pretty eager to upgrade their material transport systems, and opting for custom bucket elevators seems like a smart move. Manufacturers there are really pushing boundaries with new tech and innovative designs to create better, more reliable products.
That said, choosing the right elevator isn’t always straightforward. There’s a wide range of quality levels and specs out there, which can make things confusing. It’s super important for companies to really understand what they need beforehand. And honestly, taking lessons from what’s worked or not worked in the industry before is a huge help. When you’re making a choice, think about quality control and how long the elevator’s likely to last. Balancing your budget against what’s genuinely good quality is a key point—businesses need to weigh their options carefully before investing.
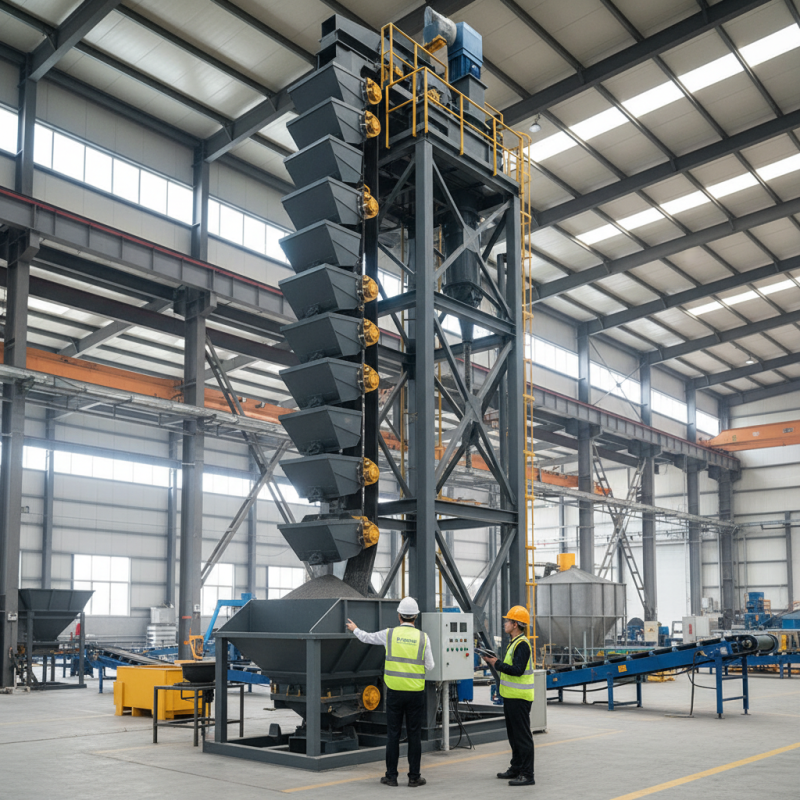
Bucket elevators play a vital role in various industries, known for their ability to transport bulk materials efficiently. The design of these elevators allows them to lift materials vertically, making them ideal for limited space environments. According to industry reports, the global bucket elevator market is projected to reach USD 3.5 billion by 2026, with a CAGR of 4.6%. This growth reflects the increasing demand for efficient material handling solutions across sectors like agriculture, mining, and manufacturing.
High-quality bucket elevators come with several key features. For example, they often use durable materials to withstand harsh conditions. Steel and plastic are common choices due to their resilience. Additionally, these elevators can be customized to fit specific height and capacity requirements. This adaptability is crucial for businesses looking to streamline operations and enhance productivity. However, improper installation can lead to operational issues, highlighting the need for professional consultation during the design phase.
Another significant advantage is their energy efficiency. Advanced models are designed to reduce power consumption, which can lead to substantial cost savings over time. Companies should consider these factors carefully when selecting equipment. Analyzing lifecycle costs from reliable sources can offer insights into long-term performance and maintenance needs. Creating a balance between initial investment and ongoing expenses is essential for making informed decisions.
| Model | Capacity (tons/hour) | Height (meters) | Material | Power (kW) | Features |
|---|---|---|---|---|---|
| Model A | 50 | 10 | Carbon Steel | 15 | Corrosion Resistant, High Efficiency |
| Model B | 75 | 12 | Stainless Steel | 18 | Durable, Low Noise |
| Model C | 60 | 14 | Aluminum | 10 | Lightweight, Easy Maintenance |
| Model D | 100 | 15 | Carbon Steel | 22 | High Load Capacity, Versatile |
Bucket elevators are essential tools for the efficient transport of bulk materials. In the market today, several types cater to different needs. The heaviness, moisture level, and type of material dictate the choice of elevator. Common types include chain bucket elevators and belt bucket elevators. Each offers unique benefits based on the operational context.
Chain bucket elevators use heavy-duty chains for high-capacity lifts. They can handle abrasive materials. Reports indicate that chain elevators dominate about 50% of the market share globally, reflecting their reliability.
Belt bucket elevators, on the other hand, are ideal for gentle handling. They are often used for lighter materials like grains and powders. Approximately 30% of installations involve belt systems.
In addition to the mechanical design, factors like material composition and speed play critical roles. Operators often face the challenge of material degradation. Regular maintenance becomes crucial for longevity. However, ensuring proper handling and integration into existing systems remains a common concern. This highlights the need for continuous education and adaptation within the industry. The data shows significant opportunities for improvement in operational efficiencies and reliability across various elevator designs.
Choosing the right bucket elevator is crucial for optimizing your material handling processes. A recent industry report indicates that inefficient bucket elevators can lead to a 30% increase in downtime. This makes it vital to evaluate your specific needs before making a decision. Factors like the type of material, flow rate, and the environment play a significant role in your selection.
When considering options, the Belt Bucket Elevator is a popular choice in many sectors. Its design is ideal for handling bulk materials efficiently and safely. However, not all belt elevators are created equal. Some may lack the durability for heavy-duty applications. A study by the International Bulk Material Handling Association highlights that improper elevator selection can significantly impact operational costs.
It’s important to reflect on the specific requirements of your project. Are you handling abrasive materials? If so, you might need a bucket elevator with enhanced wear resistance. Also, consider the space available for installation. Custom solutions may offer flexibility but could require more time and resources. Evaluating these details is vital to ensure reliability and efficiency in your operations.
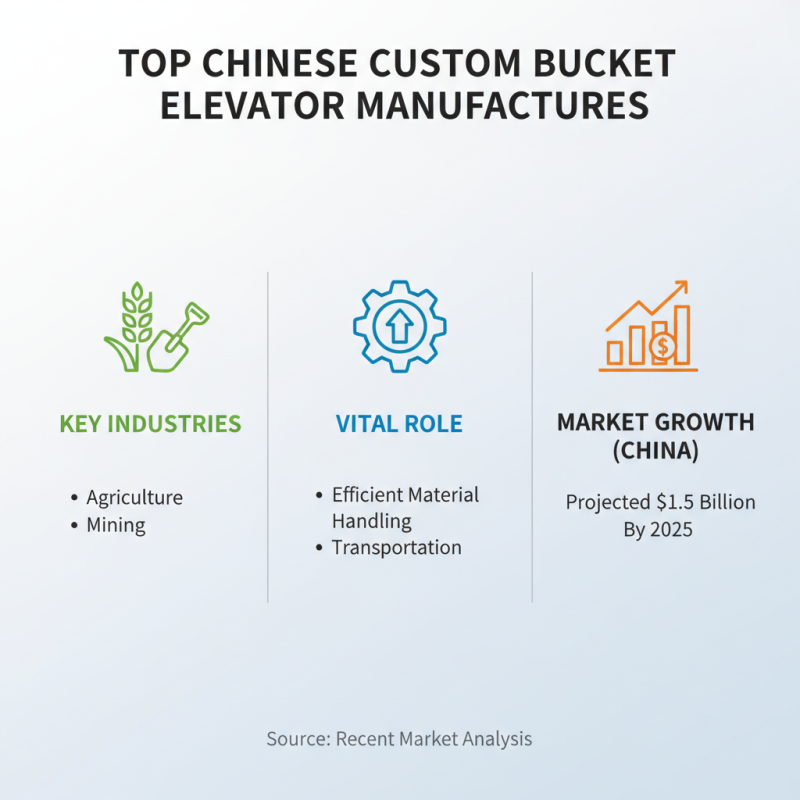
In China, custom bucket elevators play a vital role in various industries, including agriculture and mining. They are essential for efficient material handling. According to a recent market analysis, the demand for bucket elevators in China is projected to grow steadily, reaching approximately $1.5 billion by 2025. This growth reflects the increasing need for reliable transportation solutions in manufacturing processes.
Several top manufacturers in China specialize in producing high-quality custom bucket elevators. These companies leverage advanced technology and stringent quality control measures. For instance, many manufacturers use durable materials to ensure longevity and reduce maintenance needs. The focus on customization allows clients to optimize these systems for specific applications, enhancing overall productivity.
However, challenges do exist. Some manufacturers struggle with consistency in product quality. Not all components may meet the required industry standards. This inconsistency can lead to downtime and increased costs for businesses. Moreover, varying levels of expertise in installation and service support add another layer of complexity. It is crucial for buyers to choose manufacturers with proven track records and reliable customer support. Being aware of these factors can lead to better decision-making when selecting custom bucket elevator options in China.
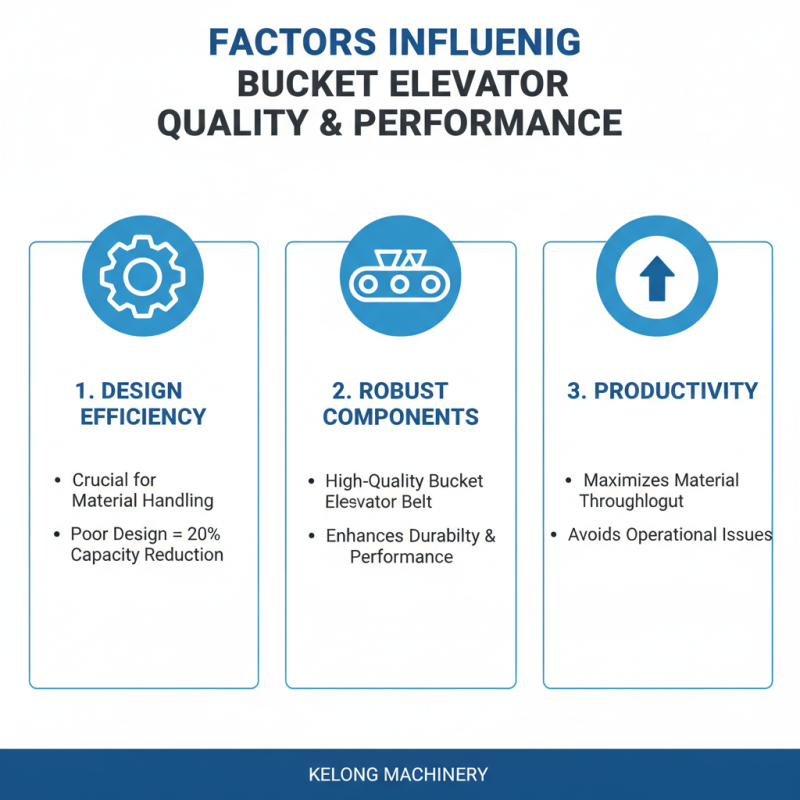
When considering high-quality custom bucket elevators, several factors greatly influence their performance and durability. The design efficiency is paramount. A well-designed bucket elevator, properly equipped with a robust Bucket Elevator Belt, significantly enhances material handling. Reports indicate that poorly designed systems can lead to a reduction in capacity by up to 20%. This inefficiency can spell trouble for operations striving for maximum productivity.
Materials used in construction also play a crucial role. Steel quality, coating, and bucket design each contribute to the overall longevity of the elevator. It is common to see premature wear in elevators that use subpar materials. In fact, maintenance costs can soar by 25% if inferior components are utilized. Regular inspections to ensure that materials meet industry standards are essential.
Tips: Always assess the bucket design’s adaptability to your specific materials. Check if the Bucket Elevator Belt can handle the load without stretching or breaking. Before any purchase, confirm the supplier’s reputation. A reliable source often translates to better quality assurance. Remember, investing in a high-quality system today can prevent costly repairs and downtime in the future.
When considering high-quality custom bucket elevators in China, cost is a crucial factor. A recent industry report highlighted that the average investment for a standard bucket elevator ranges from $30,000 to $100,000. This variation depends on customization, capacity, and design complexity. The choice of materials and technology can significantly impact the overall cost. Buckets made from durable plastic or stainless steel increase longevity but come with a higher price tag.
Maintenance costs also need attention. An efficient bucket elevator system can reduce operational downtime. According to a study, companies can save up to 25% on maintenance by selecting the right components. Additionally, high-quality Bucket Elevator Buckets are essential. They must be designed to handle specific materials without degradation. The wrong choice here can lead to deterioration and increased replacement costs, potentially negating any initial savings.
Investing in a high-quality bucket elevator requires careful planning. Potential buyers must analyze the cost versus benefits. Not everyone achieves the ideal system on the first try. Careful consideration of operational needs and long-term goals is necessary. Selecting the right supplier with experience in customized solutions can provide significant advantages. Ultimately, understanding these cost considerations will inform a smarter investment in bucket elevator technology.
This bar chart illustrates the cost considerations for high-quality custom bucket elevators in China, highlighting aspects such as capacity, material, installation, and maintenance costs. The data provided indicates a comprehensive overview for potential buyers.
Maintaining a bucket elevator is crucial for ensuring its longevity and efficiency.
Regular inspections can prevent unexpected failures. Industry data indicates that about 40% of
equipment downtime stems from maintenance issues. By following a detailed maintenance schedule, operators can increase the
lifespan of their Elevator Bucket Conveyor significantly.
One important aspect is lubrication. Ensuring that all moving parts are adequately lubricated reduces friction.
Insufficient lubrication is a common oversight. It may lead to premature wear and tear. Additionally, monitoring the
tension of belts can prevent slipping and misalignment. This can save costs in the long run.
Another critical maintenance tip involves cleaning the system.
Residue buildup can affect performance and operational efficiency. Cleaning should occur regularly. Operators should also
train staff to identify potential problems early. For example, unusual noises or
vibrations can signal underlying issues. Addressing these concerns promptly
can help in avoiding larger, costlier repairs.
: Bucket elevators are used to transport bulk materials efficiently in various industries.
Their vertical design allows effective lifting of materials, perfect for cramped environments.
The average investment ranges from $30,000 to $100,000, depending on features and customization.
Durable materials like steel and plastic are commonly used for their resilience and longevity.
Advanced models reduce power consumption, leading to significant savings over time on energy bills.
Improper installation can cause operational issues, making expert guidance essential for success.
The right components can reduce maintenance by up to 25%, minimizing downtime and costs.
Yes, choosing the wrong bucket material can lead to deterioration and increased replacement costs.
Yes, analyzing lifecycle costs helps in making informed decisions about long-term performance and maintenance needs.
Buyers must weigh costs against benefits and ensure alignment with operational goals for success.
This article explores the essential aspects of bucket elevators, emphasizing their features and advantages in material handling applications. It delves into various types of bucket elevators available in the market, providing insights on how to select the right model based on specific needs and operational requirements.
Additionally, the content highlights top manufacturers of custom bucket elevators in China, discussing the factors that influence the quality and performance of these systems. Cost considerations are addressed to help potential buyers make informed decisions. Finally, the article offers valuable maintenance tips aimed at prolonging the lifespan of bucket elevators, ensuring optimal performance and efficiency in their operations.