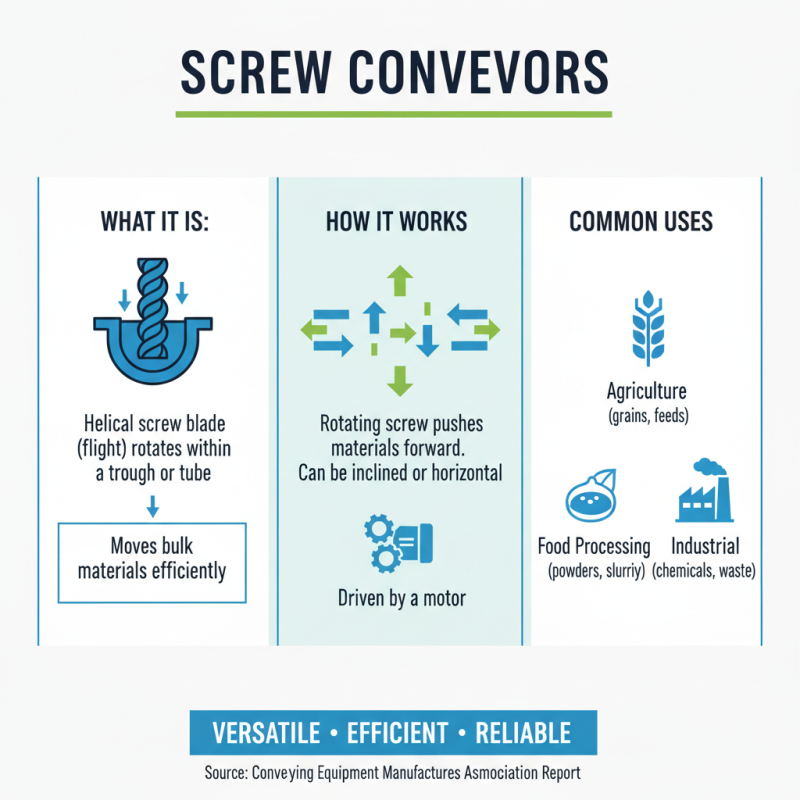
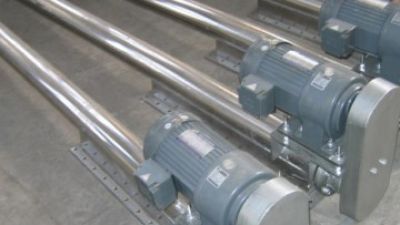
You might want to check out Screw Conveyors — they’re pretty vital in a lot of industries. Basically, they do a great job moving bulk materials quickly and smoothly. The setup is pretty straightforward: a rotating helical screw inside a sealed tube. It’s a simple design, but it gets the job done effectively, making material handling much easier.
In manufacturing, screw conveyors are like unsung heroes. They can handle all kinds of stuff—grains, powders, even slurries. That versatility is a huge plus. But, fair warning, they canWear down over time, so picking the right materials for building them is super important.
A lot of companies run into headaches around maintenance and keeping things efficient. Sometimes, if they’re not installed properly, it can lead to unexpected downtime, which nobody wants. Understanding how screw conveyors work can actually save you time and money — it really helps to get what you need based on your operational needs. At the end of the day, keeping everything running smoothly means regularly checking in and making small adjustments when needed.
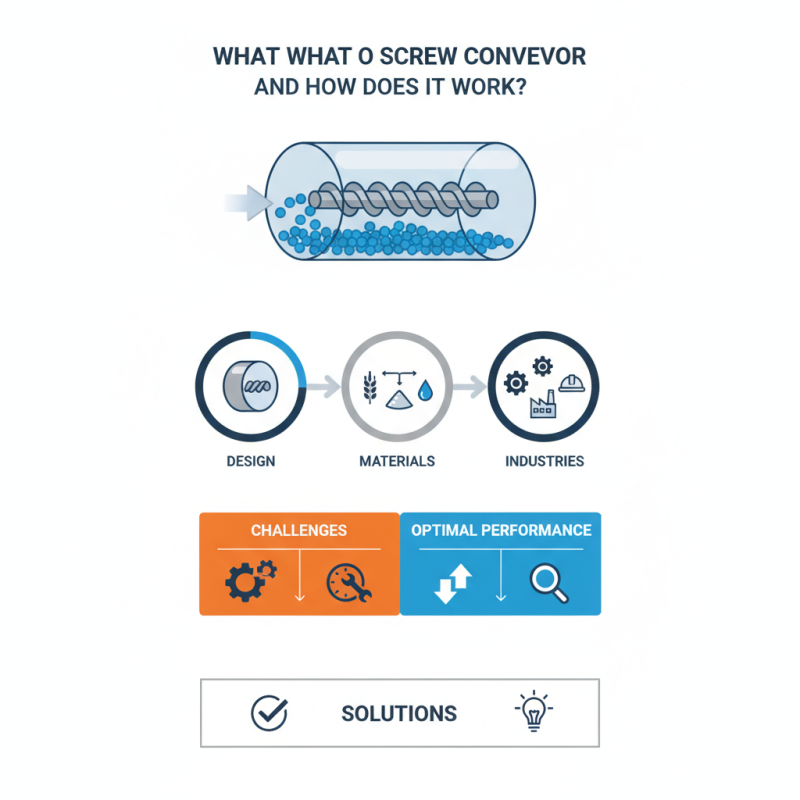
Definition of a Screw Conveyor and Its Common Applications
A screw conveyor is an essential piece of equipment in many industries. It operates using a helical screw blade, known as a flight, to move bulk materials. These conveyors can transport a variety of substances, including grains, powders, and slurries. According to a report from the Conveying Equipment Manufacturers Association, screw conveyors are often used in agriculture and food processing due to their efficiency and versatility.
Common applications of screw conveyors include mixing feed ingredients or transporting cement and chemicals. They can handle both dry and wet materials. The design allows for horizontal, inclined, and vertical transport. However, using screw conveyors may have its downsides. They can require more energy as material flow increases, leading to potential wear on the equipment over time. Addressing these issues is crucial for maintaining efficiency and reducing downtime.
Spiral Conveyors also share similarities with screw conveyors, but they often handle different materials. Both systems play critical roles in manufacturing and logistics. Operators must analyze specific needs and material properties before selecting the right type of conveyor. Misjudgment in choosing the right system can lead to inefficiencies and increased costs. Continuous assessment of usage will help overcome these challenges.
Basic Components of a Screw Conveyor: An Overview
A screw conveyor is a mechanical device used to move bulk materials efficiently. It consists of a helical screw, often enclosed in a tube. This design allows for continuous material transport, even in confined spaces. The basic components include the screw, housing, drive mechanism, and inlet/outlet ports.
The screw, usually made of durable metal, rotates around its axis. As it turns, it moves the material forward. The housing protects the screw and controls the flow of materials. At the ends, inlet and outlet ports allow easy loading and unloading.
Tips: When selecting a screw conveyor, consider the material properties. Some materials are more abrasive than others. Choosing the right material for the screw can extend its lifespan.
Packaging Conveyors often integrate screw conveyors for efficient bulk handling.
Another factor to think about is the conveyor's angle of inclination. A steep angle can cause material to slip or pack. Ensuring proper design is vital for reliable operation. Regular maintenance is necessary to avoid unexpected breakdowns. Over time, wear can change how materials flow through the system.
How a Screw Conveyor Operates: The Working Principle
A screw conveyor is a vital tool in material handling.
It consists of a helical screw, or auger, that moves bulk materials along a trough or tube.
This design allows for efficient transport of powders, grains, and other loose materials.
The screw rotates, pushing the material forward. It can work at different angles, making it versatile.
The working principle relies on the interaction between the rotating screw and the material.
When the screw turns, it creates a channel in the material. This mechanism generates movement.
The pitch of the screw, its diameter, and speed can affect transport efficiency.
If the screw is too tight, it may cause jams. Conversely, a loose screw might lead to slipping.
Screw conveyors can also be adapted for different environments.
You might find them in factories, warehouses, or even processing plants.
However, maintenance is crucial. A neglected screw conveyor can lead to breakdowns.
Regular checks on the screw and bearings can prevent this. Transitioning materials smoothly should be the goal.
But sometimes, inefficiencies crop up. Understanding these factors helps improve performance.
Types of Screw Conveyors and Their Specific Functions
Screw conveyors are vital in various industries. They transport bulk materials efficiently. Different types of screw conveyors serve specific functions. The most common types include horizontal, vertical, and inclined conveyors. Each type has unique design features to handle various materials.
Horizontal screw conveyors are often used for bulk materials like grains and powders. Their design allows for smooth product flow. According to the Conveying Equipment Manufacturers Association (CEMA), these conveyors can achieve capacities from 1 to 2,500 tons per hour. Their adaptability is a major advantage.
Vertical screw conveyors, on the other hand, raise materials from lower to higher elevations. They are more compact but can be challenging in specific situations. CEMA data suggest that they can handle materials with a maximum feeding capacity of 50 tons per hour. Inclined screw conveyors bridge the gap between horizontal and vertical. These conveyors make elevation changes smoother but require careful angle management to avoid material slippage.
Despite their advantages, each type has limitations. Horizontal conveyors may struggle with very sticky materials. Vertical conveyors can be prone to blockages if materials are not free-flowing. Understanding these nuances is essential for optimal performance.
What is a Screw Conveyor and How Does it Work? - Types of Screw Conveyors and Their Specific Functions
| Type of Screw Conveyor |
Function |
Applications |
Advantages |
| Horizontal Screw Conveyor |
Transport materials horizontally |
Food processing, agriculture |
Simple design, cost-effective |
| Inclined Screw Conveyor |
Transport materials at an incline |
Wood chips, grains |
Space-saving, versatile |
| Vertical Screw Conveyor |
Lift materials vertically |
Beverage industry, bulk material handling |
Efficient lifting, closed system |
| Screw Feeder |
Control material flow |
Packaging, manufacturing |
Precise flow control, easy integration |
| Batch Screw Conveyor |
Transport materials in batches |
Pharmaceuticals, food processing |
Controlled dosing, minimizes waste |
Advantages of Using Screw Conveyors in Material Handling
Screw conveyors are key players in material handling. They move bulk materials efficiently. One notable benefit is their ability to transport materials at various angles. The flexibility in design allows them to fit in tight spaces. According to a 2020 industry report, over 30% of manufacturers prefer screw conveyors for their versatility.
Another advantage lies in their low maintenance requirements. They have fewer moving parts than other systems. This results in less downtime and lower operational costs. A report by the Material Handling Industry of America states that installations of Screw Feeders can boost efficiency by up to 25%.
However, users must consider some drawbacks. For instance, it can be difficult to handle certain materials, such as those that tend to pack or clump. This could lead to clogging and reduced flow. Thus, knowing your materials well is crucial. Proper testing and evaluation help ensure optimal performance. When used effectively, screw feeders offer significant benefits, enhancing productivity in various industries.
Maintenance Tips for Ensuring Optimal Performance of Screw Conveyors
Screw conveyors are essential in various industries for material handling. However, their efficiency can decline without proper maintenance. Regular inspections are critical. Industry reports indicate that unmaintained equipment can suffer a performance drop of up to 30%. This impacts productivity and increases costs.
Lubrication plays a vital role in the longevity of screw conveyors. It reduces wear and tear on components. Yet, many operators overlook this simple task. According to research, a majority of failures stem from inadequate lubrication. This leads to excessive friction and potential breakdowns.
Another important aspect is monitoring operational conditions. High temperatures or humidity can affect the material flow. Reports show that these factors can lead to a decrease in performance by 15-20%. It’s essential to track these elements closely. Operators must be proactive in addressing potential issues before they escalate. Regular adjustments and alignment checks can prevent more significant problems in the long run.
Common Issues and Troubleshooting Tips for Screw Conveyors
Screw conveyors are vital for many industries. Yet, they can face common issues that impact performance. Over time, wear and tear can lead to reduced efficiency. According to industry reports, up to 30% of screw conveyor failures are due to wear. This can lead to material build-up and blockages.
An effective troubleshooting method is to inspect the screw. Look for signs of damage or corrosion. If the screws are worn, replacing them can enhance performance. Additionally, checking the feed rate and ensuring it matches the conveyor's capacity is crucial. An imbalanced feed can cause irregular flow and increased wear.
Vibration is another red flag. It often indicates misalignment or improper support. Addressing these concerns promptly can extend the life of the conveyor. Regular maintenance is essential. Keeping the system clean and lubricated minimizes issues. Remember, the Extruder Screw’s design plays a significant role in overall operation. Consistent monitoring and proactive care are key to optimal performance.
Optimizing Material Handling: The Role of Screw Conveyors in Cement and Food Industries
Screw conveyors play a pivotal role in optimizing material handling processes across various industries, particularly in the cement and food sectors. These devices are designed to efficiently transport granular, powdery, and small lump materials, making them indispensable in operations where continuous conveying is essential. The ability to handle a range of materials such as cement and food products allows for seamless integration into existing production lines, enhancing operational efficiency. According to a recent industry report, the global market for screw conveyors is expected to grow by over 5% annually, driven by their versatility and robust performance.
In the cement industry, screw conveyors are often used to connect brick extruders, facilitating a smooth transition of materials without leakage. The sealed design not only maintains the integrity of the materials being transported but also enhances safety by minimizing dust emissions. Similarly, in the food industry, the customization capabilities of screw conveyors allow for specific configurations to handle diverse food materials, ensuring compliance with hygiene standards while maximizing transfer efficiency. The operational efficiency gained from using screw conveyors can result in significant cost savings, with studies indicating that companies can reduce material waste by up to 20% through optimized handling solutions.
Moreover, the compact structure of screw conveyors ensures they fit within limited spaces, making them a favorable choice for facilities aiming to optimize layout without compromising performance. Across various applications, from chemical to mining, the adaptability and efficiency of screw conveyors are crucial in meeting the growing demands of modern manufacturing processes. Their ability to enhance safety, improve material transfer, and facilitate operational efficiency positions screw conveyors as a fundamental component in material handling systems within the cement and food industries.
FAQS
: Try restarting the application. If the issue persists, contact customer support for assistance.
Use the password recovery option on the login page. Follow the instructions sent to your email.
Yes, certain features may require a subscription or one-time fee. Check the service details for more information.
The service implements security measures. However, no system is completely secure. Remain cautious about sharing sensitive information.
Yes, you can update your profile from the account settings. Ensure that your details are accurate and current.
Document the issue and try troubleshooting. Updates or system overload may cause problems. Sharing specifics can aid support.
A mobile version may exist. Check the official website for download links and compatible devices.
You can manage notification settings in your profile options. Make sure to confirm any changes you make.
Sharing accounts can violate terms of service. It might lead to restrictions or suspension of your account.
Review your recent transactions. Contact billing support with any discrepancies you find to resolve the issue.
Conclusion
Screw conveyors are essential mechanical devices used for transporting bulk materials efficiently. They consist of a helix-shaped screw that rotates within a trough or tube, allowing for the movement of materials from one point to another. Common applications include agricultural processing, food manufacturing, and waste management. Understanding the basic components and how these conveyors operate is crucial for anyone involved in material handling.
Different types of screw conveyors serve various functions, adapting to specific needs in industries. The advantages of using screw conveyors include their ability to handle a wide range of materials, ease of installation, and minimal maintenance requirements. To ensure optimal performance, regular maintenance is key, along with being aware of common issues and troubleshooting tips. By following these guidelines, operators can maximize the efficiency and longevity of screw conveyors in their operations.